Each case study describes a real job with Maucotools machines: the component, the problem, how the on-site machining was carried out and the measurements before and after. Clients who asked for it are kept confidential.
The common thread is machining directly on the component: no disassembly, no shipping to a workshop and much shorter downtime.
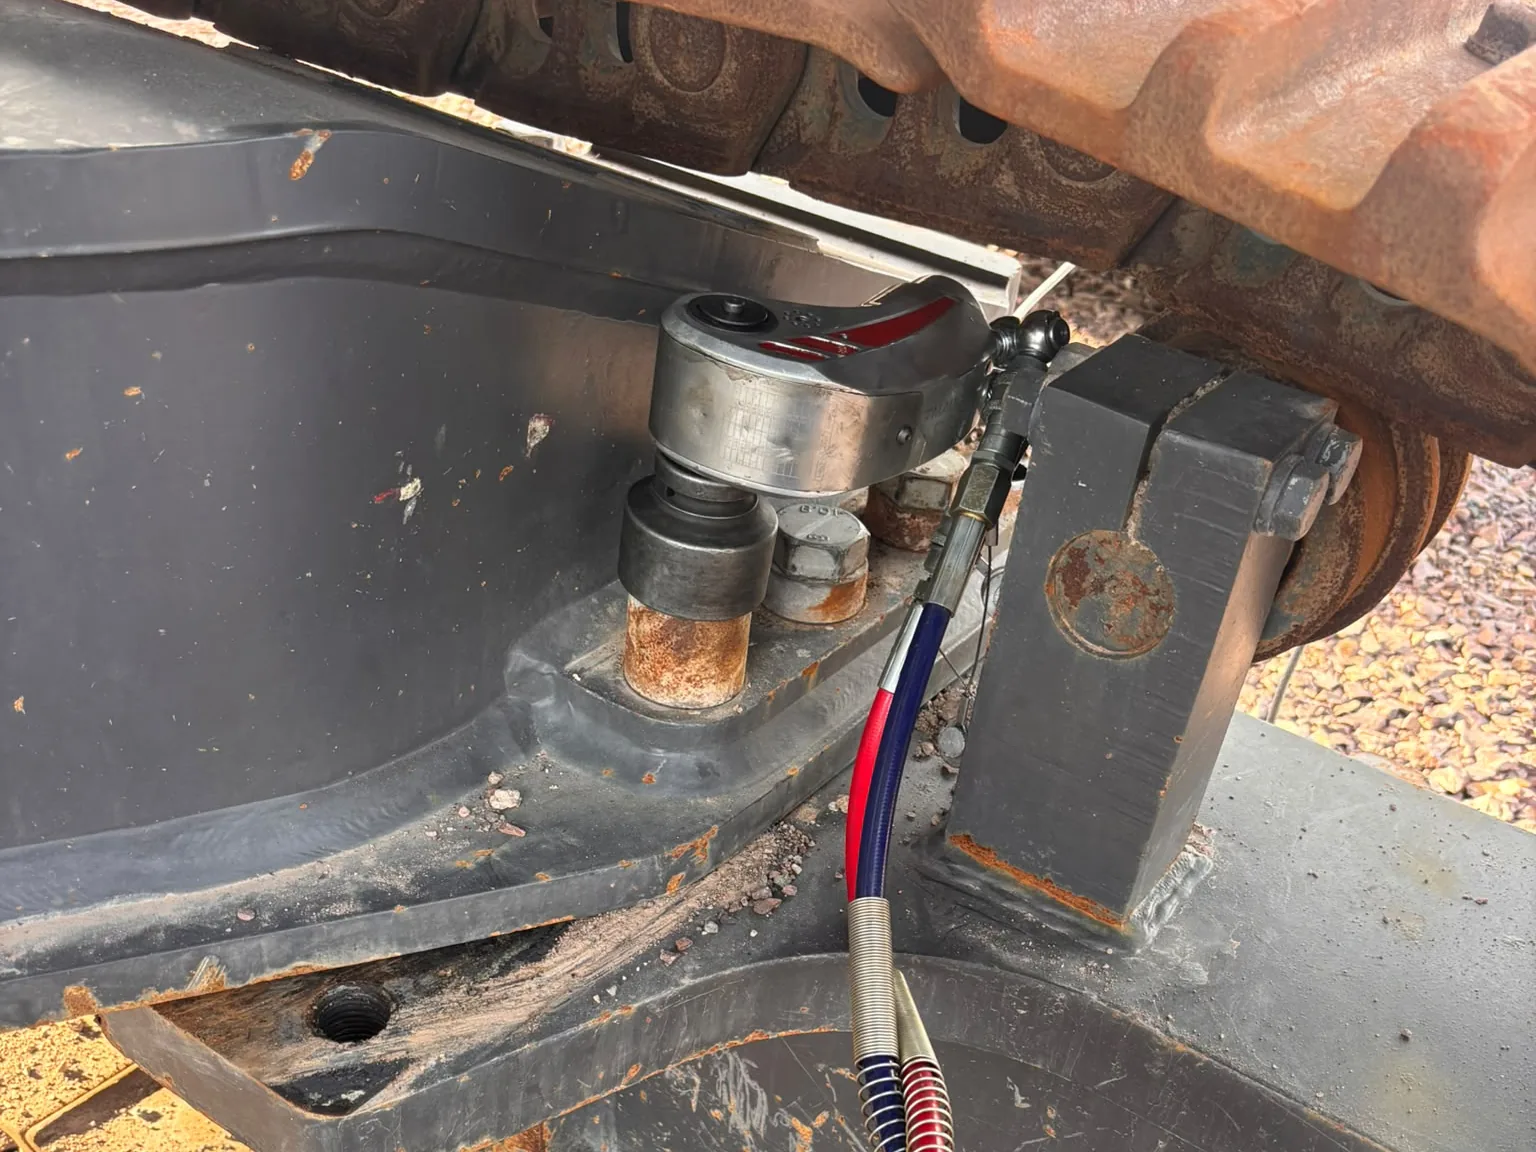
Volvo EC550 track frame removal with the MT-HTW-4500 hydraulic torque wrench
M36 bolts at 2,700 Nm on the track frames of a Volvo EC550 in the UK: controlled-torque removal with the MT-HTW-4500, one operator and a 4.2 kg tool.
- Vehicle involved
- Volvo EC550 crawler excavator, 55 t class
- Joint
- M36 bolts, specified tightening torque 2,700 Nm
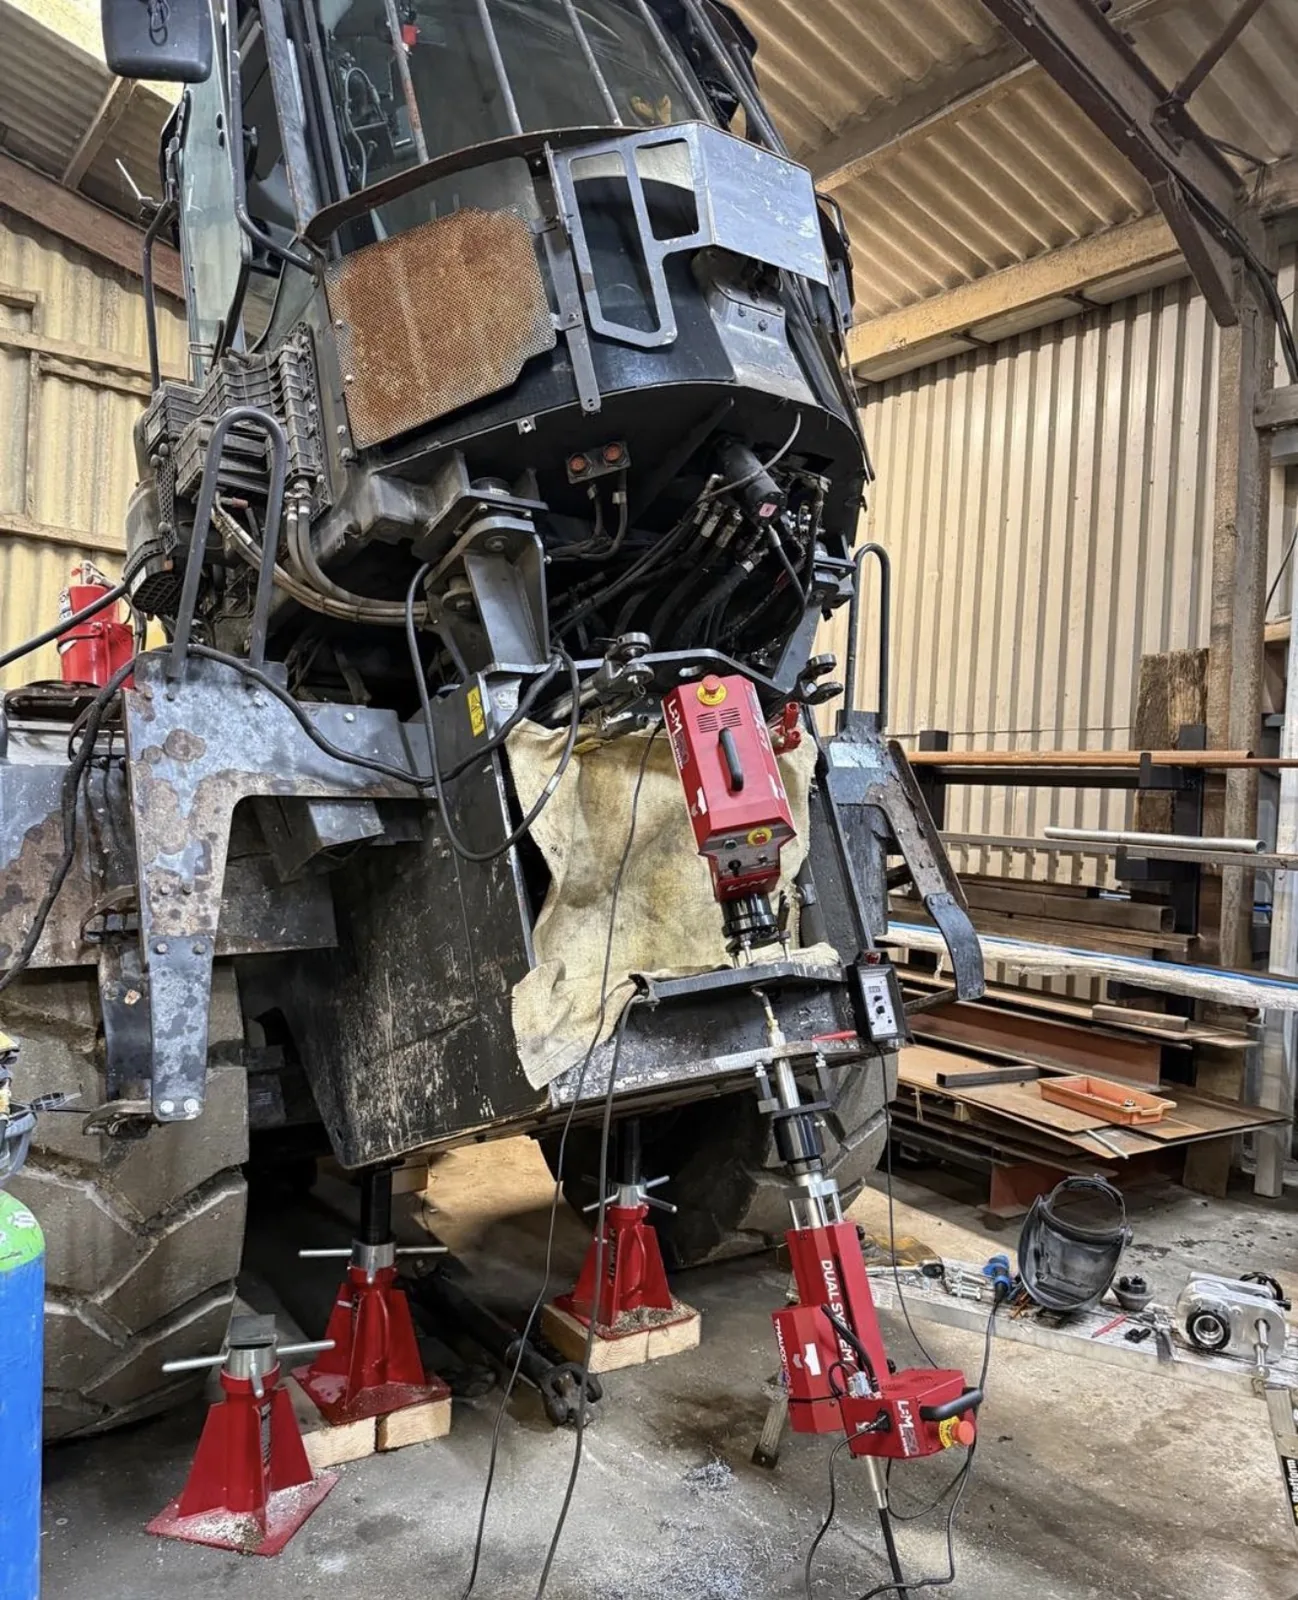
Case 821G XR centre pivot repair: bore welding and line boring in the workshop
J Hull Plant Engineers rebuilds the centre pivot bore of a Case 821G XR in its own workshop: weld overlay and line boring in one set-up.
- Vehicle involved
- Case 821G XR articulated wheel loader, approx. 18–19 t, approx. 157 kW
- Key result
- Approx. Ø150 mm bore rebuilt and machined back to size in the workshop

Bucket repair on Caterpillar 307.5
How Officina Mobile Torsani repaired the bucket of a Caterpillar 307.5 excavator, eliminating downtime with the LBM250 Dual System by Maucotools.
- Vehicle involved
- Caterpillar 307.5, earthmoving maintenance
- Key result
- Nominal tolerances restored, millimetric precision
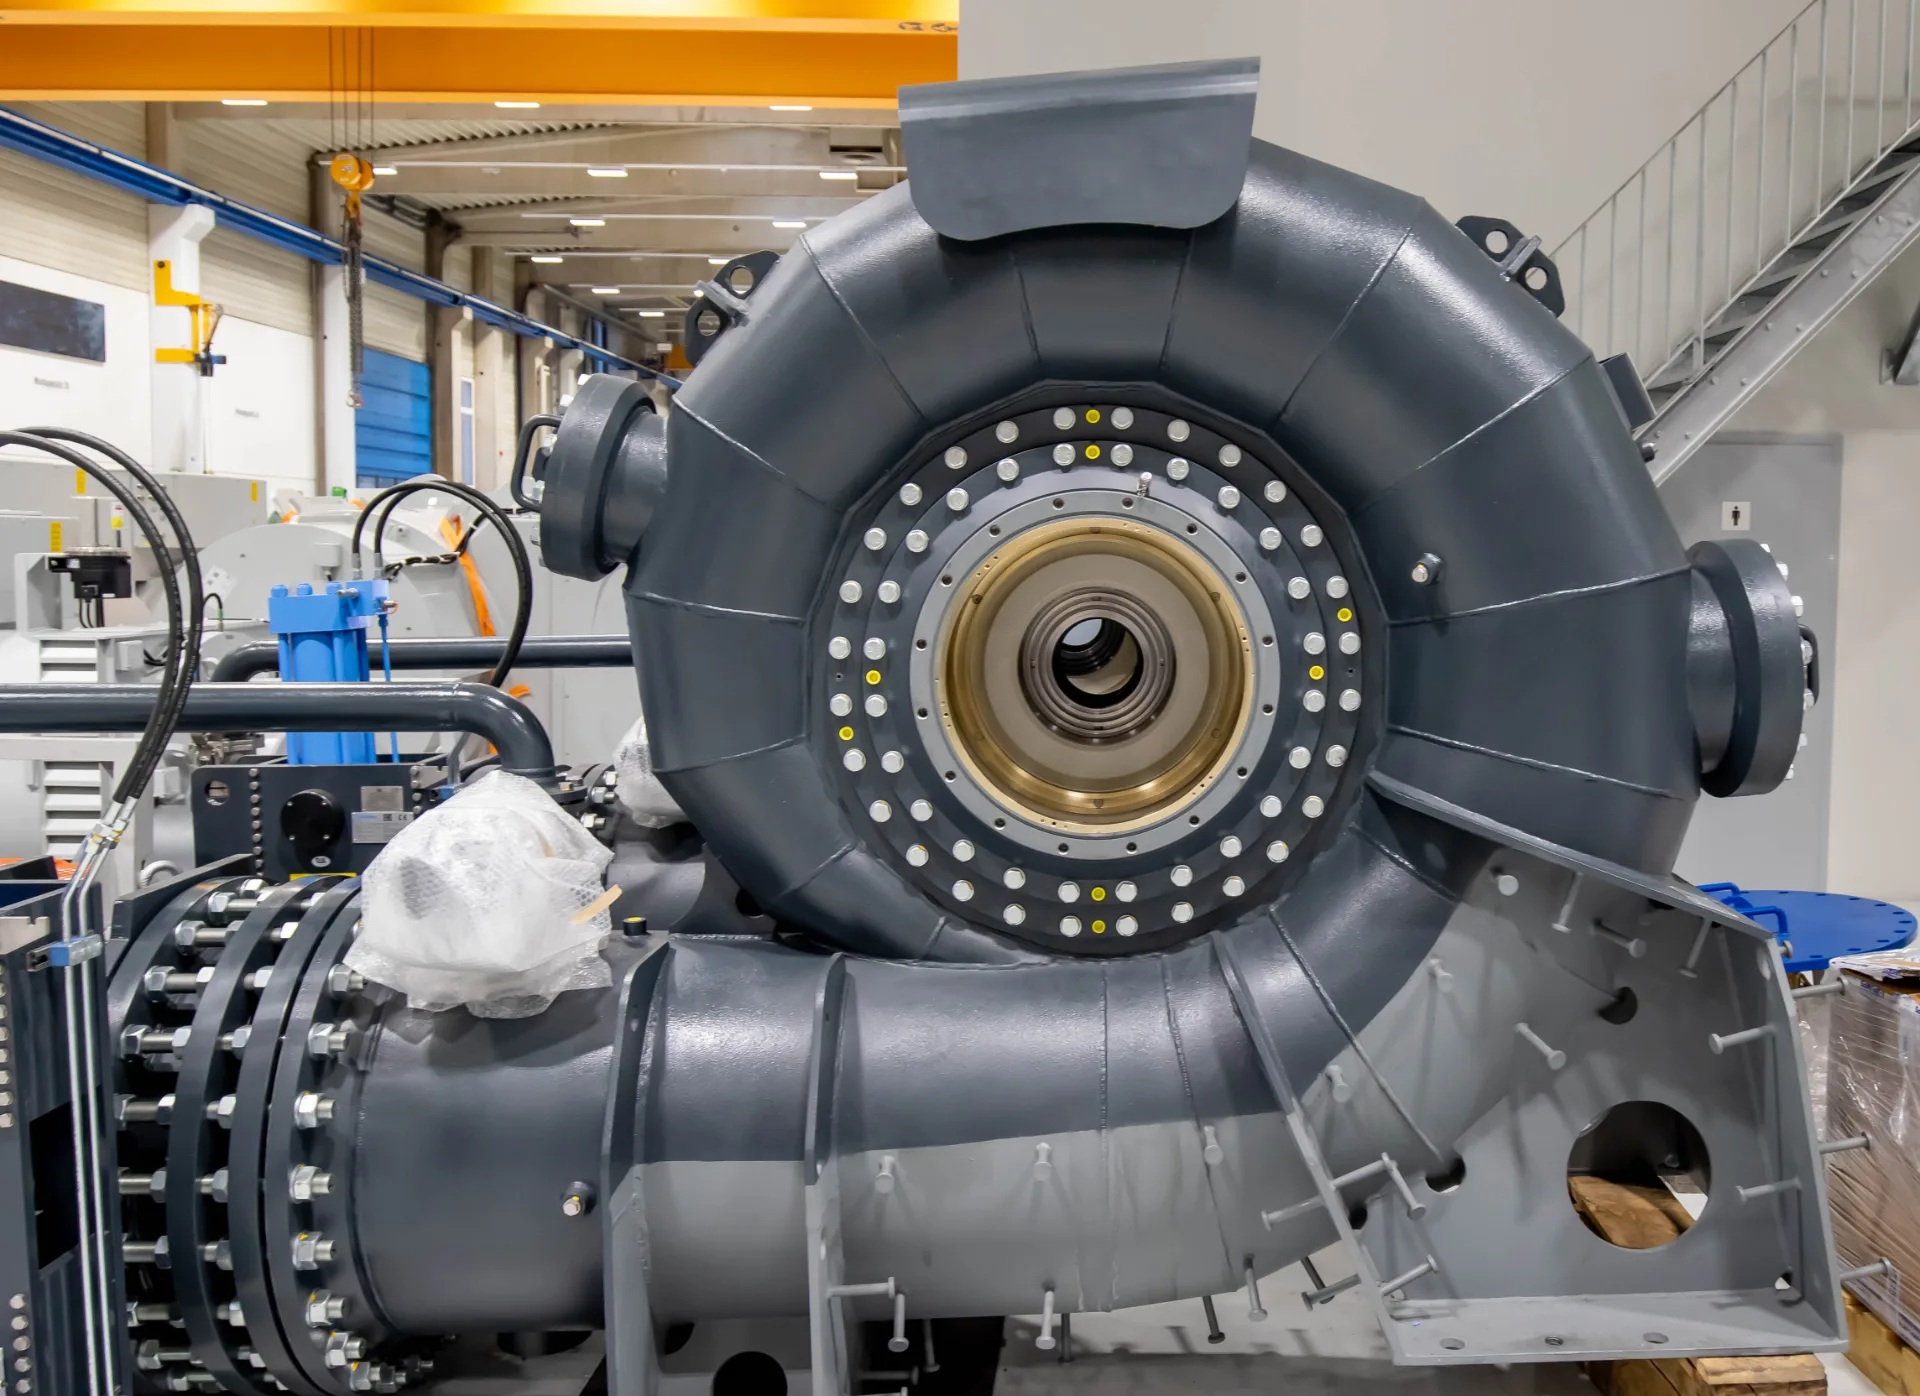
In-situ restoration of a Francis turbine guide bearing
How a hydropower operator rebuilt and re-bored the guide-bearing seat of a 12 MW Francis hydro turbine on site with the LBM600 Dual System, bringing the unit back online in two days instead of weeks.
- Plant
- 12 MW Francis turbine, run-of-river hydro plant
- Result
- Ø510 H7 seat restored, ~€45,000 saved
Measured results
Dimensions before and after the job, as reported in each case.
| Case | Measurement | Before → after | Outcome |
|---|---|---|---|
| Volvo EC550 track frame removal with the MT-HTW-4500 hydraulic torque wrenchMT-HTW-4500 | M36 bolts | 2,700 Nm | Controlled torque, no makeshift levers or impact wrenches |
| Operator | Just one | With a 4.2 kg tool | |
| Torque headroom | ~60% | The required 2,700 Nm against the MT-HTW-4500's 4,511 Nm maximum | |
| Case 821G XR centre pivot repair: bore welding and line boring in the workshopLBM250 DUAL SYSTEM | Centre pivot bore | approx. Ø150 mm | Rebuilt and machined back to size in the workshop |
| Weld overlay and boring | Single set-up | No re-centring between the two steps | |
| Repair | Complete repair | Bore rebuilt, not just the bearing replaced | |
| Organisation | In-house | Job handled with the workshop's own machine | |
| Bucket repair on Caterpillar 307.5LBM250 DUAL SYSTEM | Large hole | 80.60 → 80.05 mm | Geometry recovery |
| Bushing | 79.60 → 80.00 mm | Perfect coupling | |
| Pin hole | 45.60 → 45.15 mm | Restored | |
| In-situ restoration of a Francis turbine guide bearingLBM600 DUAL SYSTEM | Seat restored | Ø512.4 → 510.00 mm H7 | Geometry recovered |
| Ovalization | < 0.02 mm | Concentricity restored | |
| Plant downtime | 3 weeks → 2 days | Unit back on the grid |
How an on-site job works
- 01
Survey of the dimensions and wear of the bores on the component.
- 02
Mounting the line boring machine on the component, aligned to the original axis.
- 03
Weld overlay where material is worn, with the same Dual System machine.
- 04
Boring to size and final tolerance check.
Have a similar component to restore? Estimate the savings or ask for a technical opinion.